Key takeaways
- Binder at 3–8% holds the pan; too little crumbles, too much will not pick up.
- Press force and dwell time control density and pan hardness.
- Breakage in transit is a pack problem as often as a formula problem.
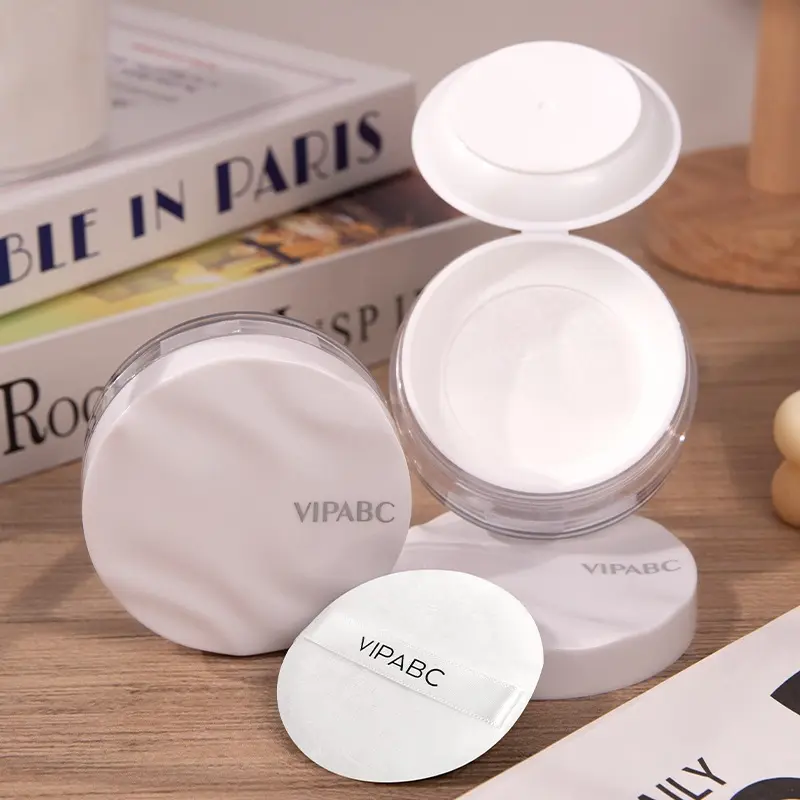
A pressed powder is a loose powder blend with a binder, compacted into a pan under pressure. The binder holds the particles together and the press force sets the density; together they decide whether the pan is hard enough to survive a handbag and soft enough to pick up on a brush. Both extremes are common and both are expensive.
1. Binder chemistry
Dimethicone, a fatty ester or a silicone wax at 3 to 8 percent is the usual binder. Oil-based binders give a soft, creamy pan; silicone binders give a harder pan with better water resistance. The binder also changes the finish, so it is a texture decision as well as a structural one.
2. Binder distribution
The binder must be distributed evenly or the pan has soft and hard zones that fail at different times. High-shear mixing after binder addition is standard, and the mixing time belongs in the batch record. A pan that breaks in one corner and not another has a distribution problem.
3. Press force
Typical press forces run 1 to 5 tonnes for a 57 mm pan. Higher force gives a denser pan that survives transit and resists pick-up; lower force gives a softer pan that applies generously. The correct force depends on the filler: a talc-based blend needs less than a mica-based one.
4. Dwell time
Dwell time, the period the force is held, matters as much as the peak force. A short dwell at high force produces a pan that rebounds and cracks; a longer dwell at lower force produces a more uniform pan. Set both in the specification rather than only the tonnage.
5. Pan hardness testing
Pan hardness is measured with a penetrometer or a three-point bend test. The practical target is a pan that resists a thumb press but yields to a brush. Without a number, approval is subjective and every batch is argued about.
6. Breakage in transit
Pressed powders break in transit at 2 to 5 percent without a protective insert. A foam or a moulded pulp insert reduces it to under 1 percent. The insert costs a few cents and the returns cost far more, which is a decision that should be made before the carton is designed.
7. Talc, mica and the press
Talc compacts easily and gives a hard, flat pan. Mica compacts poorly because its plates align and split, which is why mica-heavy pans need more binder and a lower force. A talc-free pressed powder is a different pressing problem, not the same one with a substituted filler.
8. Hygiene and repressing
Pressed powder is a dry product but not a sterile one. The press tool must be cleaned between shades, and a repressed pan must not reuse powder from the press tray without sieving. Cross-shade contamination shows up as a speck on a light shade, which is the complaint that gets photographed.
9. The shade test
Pressing changes the appearance of a shade: a compacted powder reads darker and more opaque than the same loose blend. Approve the shade on the pressed pan under standard light, not on the loose powder, or the first production run will look wrong against the lab sample.
10. Stability
A pressed pan is tested for drop resistance, pan hardness and shade after twelve weeks at 40 degrees. Some binders migrate at high temperature and leave a hard skin on the surface that will not pick up. That failure is invisible at release and obvious in the market, so pull at four weeks.
11. Where it fits
Pressed formats sit in the setting powder range; the loose comparison continues in the loose versus pressed entry.
Reference: Pressing trials and transit test results, 2025